Industrial Export Packaging Built for Real Manufacturing and Logistics
Industrial products are not forgiving.
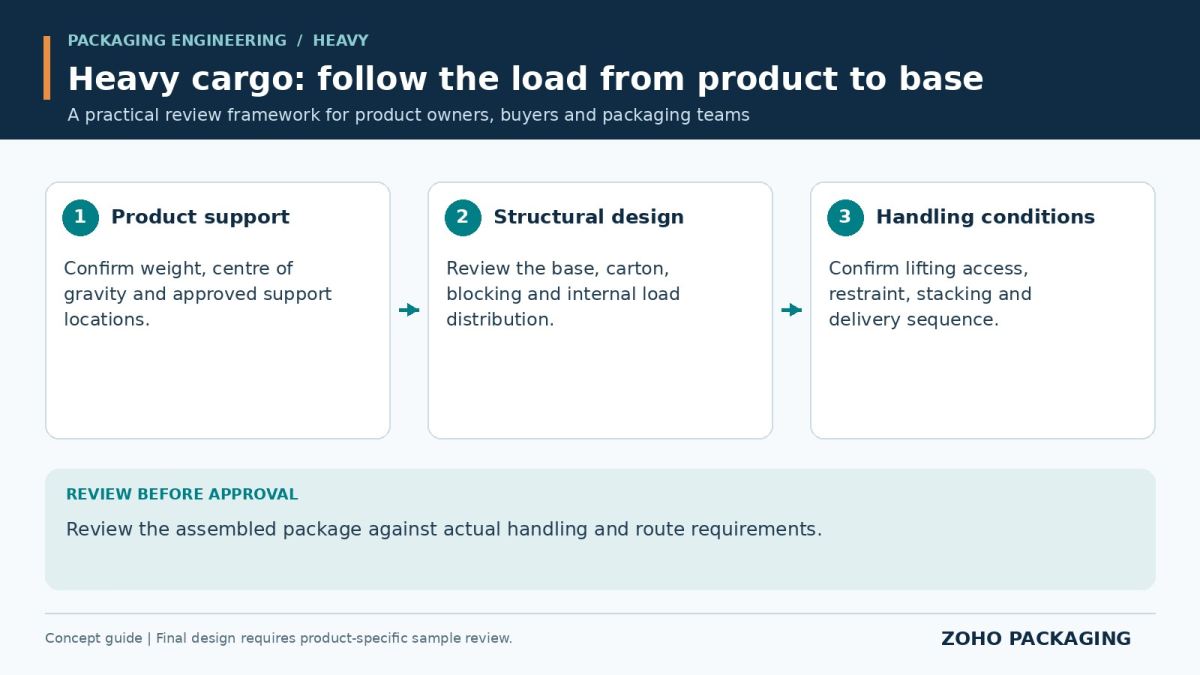 Review the assembled package against actual handling and route requirements.
They are:
- heavy
- complex
- high-value
- difficult to replace
Industrial export packaging must handle load, shock, vibration, and environmental stress — while remaining efficient for large-scale operations.
At Zoho Packaging, we design packaging systems for industrial reality, not theoretical conditions.
Why Industrial Packaging Requires a System Approach
Industrial packaging is not just about a box.
It is about:
- product protection
- logistics efficiency
- handling safety
- cost control
Without proper design, companies face:
- frequent damage
- inefficient shipping
- increased operational cost
- inconsistent packaging quality
Core Principles of Industrial Export Packaging
1. Structural Strength for Heavy Loads
Industrial products require:
- high compression strength
- reinforced structure
- load distribution design
We engineer packaging that can handle real weight, not just estimated load.
2. Shock & Vibration Protection
Industrial goods are often sensitive to:
- impact during handling
- vibration during long-distance transport
We integrate:
- cushioning systems
- structural shock absorption
- vibration control design
3. Internal Fixation & Stability
Movement is a major risk.
We design:
- blocking systems
- custom supports
- fixed positioning
4. Environmental Resistance
Export conditions include:
- humidity
- temperature changes
- long exposure time
We incorporate:
- moisture-resistant design
- protective layers
- environment-adapted materials
5. Pallet & Container Integration
Industrial packaging must work with logistics.
We optimize:
- pallet layout
- container loading
- handling efficiency
Industrial Packaging vs Standard Packaging
| Factor |
Standard Packaging |
Industrial Packaging |
| Load capacity |
Limited |
High |
| Design approach |
Generic |
Engineered |
| Protection level |
Basic |
Advanced |
| Logistics integration |
Minimal |
Optimized |
| Consistency |
Variable |
Controlled |
Common Industrial Packaging Failures
- structural collapse under heavy load
- product movement during transport
- damage from vibration and impact
- poor pallet alignment
- inefficient container utilization
👉 These failures increase cost and reduce reliability.
Industrial Sectors We Support
Manufacturing equipment
→ heavy + structural support
Automotive parts
→ impact protection + anti-scratch
Electronics manufacturing
→ precision + anti-vibration
Metal and hardware products
→ load + surface protection
Energy and infrastructure components
→ large scale + high durability
Industrial Packaging = Operational Efficiency
Industrial packaging is not just protection.
It improves:
- handling speed
- warehouse efficiency
- shipping consistency
- scalability
👉 Especially for high-volume operations.
Reduce Risk, Improve Performance
Industrial export packaging helps:
- reduce damage rate
- improve delivery reliability
- lower total cost
- support long-term operations
Our Industrial Packaging Approach
We design based on:
- product characteristics
- load requirements
- shipping conditions
- logistics system
- production consistency
We provide:
- heavy duty export packaging
- custom industrial packaging systems
- pallet-integrated solutions
- shockproof and moisture-resistant design
- packaging optimization for cost and efficiency
Built for Industrial Scale
Industrial packaging must perform across:
- factories
- warehouses
- shipping containers
- global supply chains
At Zoho Packaging, we build packaging systems that scale with your business.
Because:
👉 Industrial packaging is not just protection.
It is part of your operation.
FAQ
1. What is industrial export packaging?
Industrial export packaging refers to packaging solutions designed for heavy, complex, and high-value industrial products. It focuses on strength, protection, and logistics efficiency.
2. Why is industrial packaging different from standard packaging?
Industrial packaging must handle heavier loads, more complex products, and longer shipping distances. It requires engineered solutions rather than standard designs.
3. What industries need industrial packaging?
Manufacturing, automotive, electronics, energy, and heavy equipment industries all require industrial packaging solutions.
4. Can industrial packaging reduce damage?
Yes. Proper design minimizes movement, absorbs shock, and ensures structural stability, reducing damage risk.
5. How does industrial packaging affect cost?
It reduces total cost by preventing damage, improving efficiency, and optimizing logistics.
6. What is the biggest mistake in industrial packaging?
Using standard packaging without considering product weight, structure, and shipping conditions.
7. Can corrugated packaging be used for industrial products?
Yes, with proper design. Reinforced corrugated packaging can handle many industrial applications.
8. How does pallet design impact industrial packaging?
It affects load stability, handling efficiency, and shipping performance.
9. What risks do industrial products face during shipping?
Impact, vibration, moisture, and handling stress are the main risks.
10. How do you design industrial export packaging?
By analyzing product characteristics, logistics conditions, and risk factors to create a tailored solution.